Finite element simulation with Drucker-Prager/Cap (DPC) model is commonly used to conduct numerical modeling of the compression of granular material. In the pharmaceutical field, this model is increasingly used for the numerical simulation of the process of die compaction.
The compression curve, obtained from die compaction process, consists of three parts: the loading part (compression phase), the unloading part (decompression phase) and the ejection phase. Commonly the axial stress (applied stress) as a function of the tablet thickness and the radial transmission (radial stress versus axial stress) curves are studied. In addition of the compression curves, the numerical modeling makes it possible to analyze the spatial distribution of the density and the stresses.
To perform numerical simulation with DPC model, the model parameters must be determined. Usually die compaction test is used to make compacts and, during the compression, data are recorded. The compacts are then treated and submitted to at least two failure tests, and new data are collected. The data obtained from die compaction and failure tests make it possible to determine the DPC parameters.
Depending on the method used, the instrumentation of the devices or the accuracy of the measures, the data obtained from the experimental tests for the characterization of the model parameters may vary from one study to another. For granular materials like pharmaceutical powders, this variation can be important and the consequences on the final result must be studied. In this work, the influence of the plastic and elastic parameters on the numerical results during the compression and the decompression phases will be discussed.
Influence of plastic parameters of DPC model
The DPC model is commonly presented in the p-q plan (p: hydrostatic stress and q: Mises equivalent stress). In this plan, the failure surface of the model consists of two principal parts: the failure line (Fs) and the cap surface (Fc).
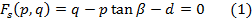
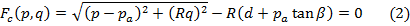
For the failure line, the parameters to characterize are the powder cohesion d and the friction angle b. The cap parameters (hydrostatic pressure pa, cap eccentricity R and hydrostatic yield pressures pb) are calculated from d and b. Thus the variation of R, pa and pb is due to the variation of d and b. The parameters of the failure line are usually characterized by using diametral and uniaxial compression tests. Eq.1 can be expressed as a function of failure strengths obtained from diametral (sd) and uniaxial (su) compression tests and d and b can be calculated as:
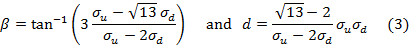
All these parameters were characterized by experimental tests and represent the reference values in this work. Eq.3 shows that potential variations of b and d are necessarily due to variations of su and sd. Thus, in the proposed work, variations of ±53% were applied to su and sd. These variations were applied in order to cover a broad range of the friction angle values of microcrystalline cellulose (MCC) found in the literature. Five cases were studied: the reference case (sd, su) and four other cases: (sd +,su +), (sd -,su +), (sd +,su -) and (sd -,su -) with (sd ±=sd ±0.53sd and su ±=su ± 0.53su). The corresponding values of b and d were then calculated.
Numerical simulations were conducted with variations of the friction angle and the powder cohesion for the five cases cited above. The plot of the axial stress as a function of the tablet thickness shows that the curves obtained from the five cases are identical. The curves of radial stress versus axial stress are also the same. Thus, during the compression and the decompression phases, variations of the friction angle and/or the cohesion of the powder have no influence on the evolution of these output variables.
Since the variation of the failure line has no influence on the results during the compression and decompression phases and the characterization of its parameters requires additional experimental tests, an alternative model like the modified Cam-Clay (MC-C) model can be used to simulate the compaction. The MC-C model is simple to use and requires less experimental tests for the parameter characterization. The yield surface has the shape of half an ellipse in the p-q plan. The equation of the yield surface (yield function F) is defined as:
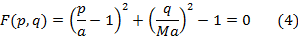
Where a is the size of the yield surface and M is a material constant.
Comparison between DPC and MC-C models
DPC and MC-C models were used to simulate the powder behavior during die compaction process. The curves of axial stress pax versus tablet thickness obtained from MC-C and DPC models are superimposed. The radial transmission obtained from MC-C model is identical to that obtained from DPC model. These comparisons show that the simulation with the two models gives the same result.
The axial stress distributions are the same for the two models at the maximum of compression and at the end of decompression. The same result was found for the relative density distribution. It is clear that the MC-C model is able to predict the powder behavior during the compression as well as the DPC model.
Influence of elastic parameters of DPC model
Variations of ±20% on the values of Young’s modulus E and Poisson’s ratio n obtained from experiments were applied. This makes it possible to cover a broad area of the values of E and n found in the literature for the numerical modeling of MCC powder with DPC model.
Nine configurations were studied: the configuration with reference values of E and n (reference case), the cases E-, E+, n-, n+ (with variations of ±20% on only one of the two parameters) and the cases E-n-, E+n+, E-n+ and E+n- (with variations of ±20% on both parameters). E varies from 0.14 to 1.9 GPa at -20% and from 0.21 to 2.8 GPa at +20%. n is between 0.18 and 0.32 at -20% and between 0.26 and 0.48 at +20%. In comparison to the elastic properties found in the literature, these variations are realistic. The numerical curves (axial stress versus tablet thickness and radial stress versus axial stress) for all the configurations (Ref, E-, E+, n-, n+, E-n-, E+n+, E-n+ and E+n-) were analyzed.
Influence of Young’s modulus
The variation of Young’s modulus E (Poisson’s ratio was kept constant) leads to a change of the axial stress versus tablet thickness curve. The difference appears at the beginning of the powder hardening and remains until the end of the compression phase. During the decompression phase, this difference decreases and disappears at the end of the decompression. As a consequence, the change of E has no influence on the final tablet thickness.
The variation of Young’s modulus E has no influence on the radial transmission curve. The influence of E was also assessed at a local scale by comparing the distributions of the relative density, the axial and radial stresses at the maximum of compression and at the end of the decompression. The distributions are always identical which means that E has no effect on these output variables at the local scale.
Influence of Poisson’s ratio
The influence of Poisson’s ratio n gradually appears during the powder hardening (during plastic deformation) and is maximal at the end of the compression phase. For a same compression pressure, the tablet thickness is lower when a small Poisson’s ratio is used. During the decompression phase the effect of Poisson’s ratio slightly decreases but the final tablet thicknesses remains clearly different.
Concerning the radial transmission, at low pressure, the variation of n does not lead to a change of the die wall pressure (radial stress). When the applied pressure is high enough (up to 120 MPa), the die wall pressure increases with n. At the end of the decompression, a small Poisson’s ratio gives a high residual die wall pressures (RDP) and the increase of n leads to a decrease of the RDP.
The distribution of the relative density does not change when Poisson’s ratio varies. The same result was found for the distribution of the axial stress at the maximum of compression. For the distribution of the radial stress at the maximum of compression, a slight difference is observed. The stress distribution at the end of the decompression phase is completely dependent on Poisson’s ratio. With small Poisson’s ratio, the residual stress is high and it is low when n is high.
This study shows that the influence of Poisson’s ratio n is more important than that of Young’s modulus. The influence of n is shown to be less important on the MDP than on the RDP. As a consequence, an underestimation of Poisson’s ratio may not show a difference in the MDP but may strongly overestimate the RDP. In addition the occurrence of capping is correlated to the RDP. Thus, when studying capping problem with FEM modeling during die compaction, Poisson’s ratio is an important parameter and must be characterized with accuracy.
See more of this Group/Topical: Handling & Processing of Granular Systems